
Roll Cleaning
Roll Technology has provided acid cleaning services for heat transfer roll applications for over 20 years. Most rolls we service are clogged with calcium deposits caused by poor plant or city water quality, or by aging filtration systems that have become less effective over time.
When heat transfer rolls (both heating and cooling) cannot maintain a consistent temperature across the face, and your web is sticking to the roll surface (commonly called "hot spots"), internal vibratory acid cleaning is often the solution.
Inhibited acid cleaning removes calcium, carbon, and scale deposits that build up in the flow channels of heat transfer rolls, restricting fluid flow and causing temperature variation across the roll face. Our process incorporates a vibrating sequence to loosen internal deposits that chemical treatment alone may not reach. We use high-speed pumps and measure GPM flow readings before and after every cleaning cycle.
AAcid cleaning is most effective as a preventive maintenance step, addressing deposits before "hot spots" develop into serious heat transfer problems. If your cooling water system is prone to calcium buildup, or your hot oil rolls are accumulating carbon deposits, regular acid flushing helps maintain thermal performance and extend roll life.
Upgrading Services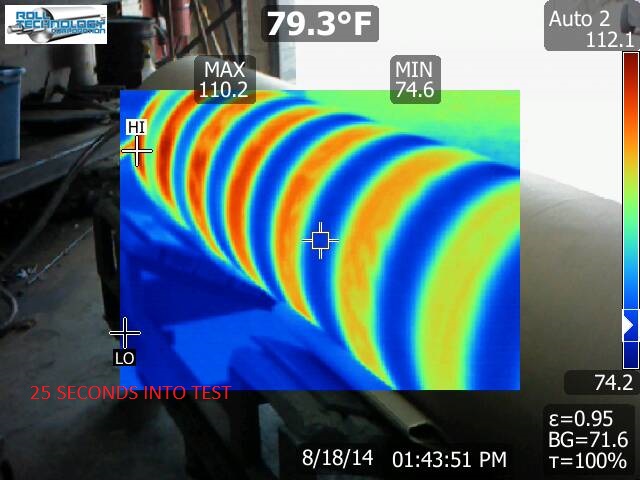
Roll Technology is constantly striving to improve its services and we have recently upgraded our acid cleaning heat roll service. We now take thermal imaging pictures of the rolls internals before flushing and after flushing - showing the difference in the rolls fluid flow. We have also added a vibrating technique while the roll is being flushed to further loosen the calcium deposits and/or carbon deposits and scale buildup.
Before any acid cleaning begins, we require the MSDS sheet for the fluid running through your rolls. Certain materials are incompatible with the acids used in our process and can create fume or waste treatment problems. All waste from our facility is monitored by the local Regional Sewer Authority, including hexavalent chromium rinse water from our hard chrome plating operations.
For acid cleaning on hot oil roll applications, we ask customers to drain all oil before shipping the roll to our facility. We then clean the roll with a hot soap solution to remove oil residue and expose the underlying carbon buildup. An inhibited acid flush runs through the inner flow channels for three to four days, with continuous vibration to shake loose carbon particles and debris. Thermal images and GPM flow meter readings taken before and after cleaning document the improvement in heat transfer performance.
To learn more about Acid Cleaning, contact us today!
Signs Your Heat Transfer Rolls Need Acid Cleaning
Inconsistent temperature across the roll face is the most common indicator that internal flow channels are restricted. Operators often notice this as "hot spots" where the web sticks to the roll surface, leading to product defects and unplanned downtime. Other signs that acid cleaning is needed include:
- Gradual decline in thermal performance despite steady fluid input temperatures
- Increasing temperature differential readings across the roll face
- Visible calcium or scale deposits in fluid lines connected to the roll
- Reduced GPM flow rates compared to baseline measurements
- Web quality issues that cannot be traced to surface condition
If your rolls show any of these symptoms, a roll inspection can confirm whether internal deposits are the cause before scheduling an acid cleaning cycle.
How Acid Cleaning Fits With Other Roll Maintenance Services
Acid cleaning restores internal flow and thermal performance without removing material from the roll surface, making it an ideal first step before other roll maintenance work. Many customers pair acid cleaning with precision roll grinding to restore surface geometry, or hard chrome plating to rebuild the wear surface. Starting with clean internal channels means any subsequent surface work performs as designed, because the roll can hold its target operating temperature from the start.
For rolls with both internal deposit issues and external surface wear, our team can coordinate acid cleaning, grinding, plating, and roll finishing in a single trip to our Greenville, SC facility. This eliminates multiple shipments between vendors and gets your rolls back into production faster. If the roll has sustained damage beyond surface wear, our roller repair team evaluates whether restoration is viable before any additional work begins.
Frequently Asked Questions About Acid Cleaning
What types of deposits does acid cleaning remove?
Acid cleaning removes calcium deposits caused by hard water or poor filtration, carbon deposits from hot oil systems, and general scale buildup that accumulates in the internal flow channels of heat transfer rolls over time.
What does the acid cleaning process include?
Our process uses inhibited acid flushed through the roll's internal flow channels with high-speed pumps. A vibrating sequence runs during the flush to loosen deposits. We take thermal images of the roll's internals before and after cleaning and measure GPM flow readings at both stages to document results.
Why should acid cleaning be done before heat transfer problems develop?
Acid cleaning is most effective as a preventive measure. If your cooling water system is subject to calcium deposits or your hot oil system is producing carbon buildup, regular acid flushing helps maintain thermal performance and extend roll life before "hot spots" develop into larger heat transfer issues.
How often should I schedule acid cleaning?
It depends on your water quality, fluid type, and operating conditions. Rolls running on high-mineral water typically need cleaning every 12 to 18 months. We establish baseline flow and thermal readings after each cleaning so you can track when performance starts to decline and schedule the next cycle accordingly.
CONTACT US TODAY
Click HERE to request a quote or call us at 864.269.7703